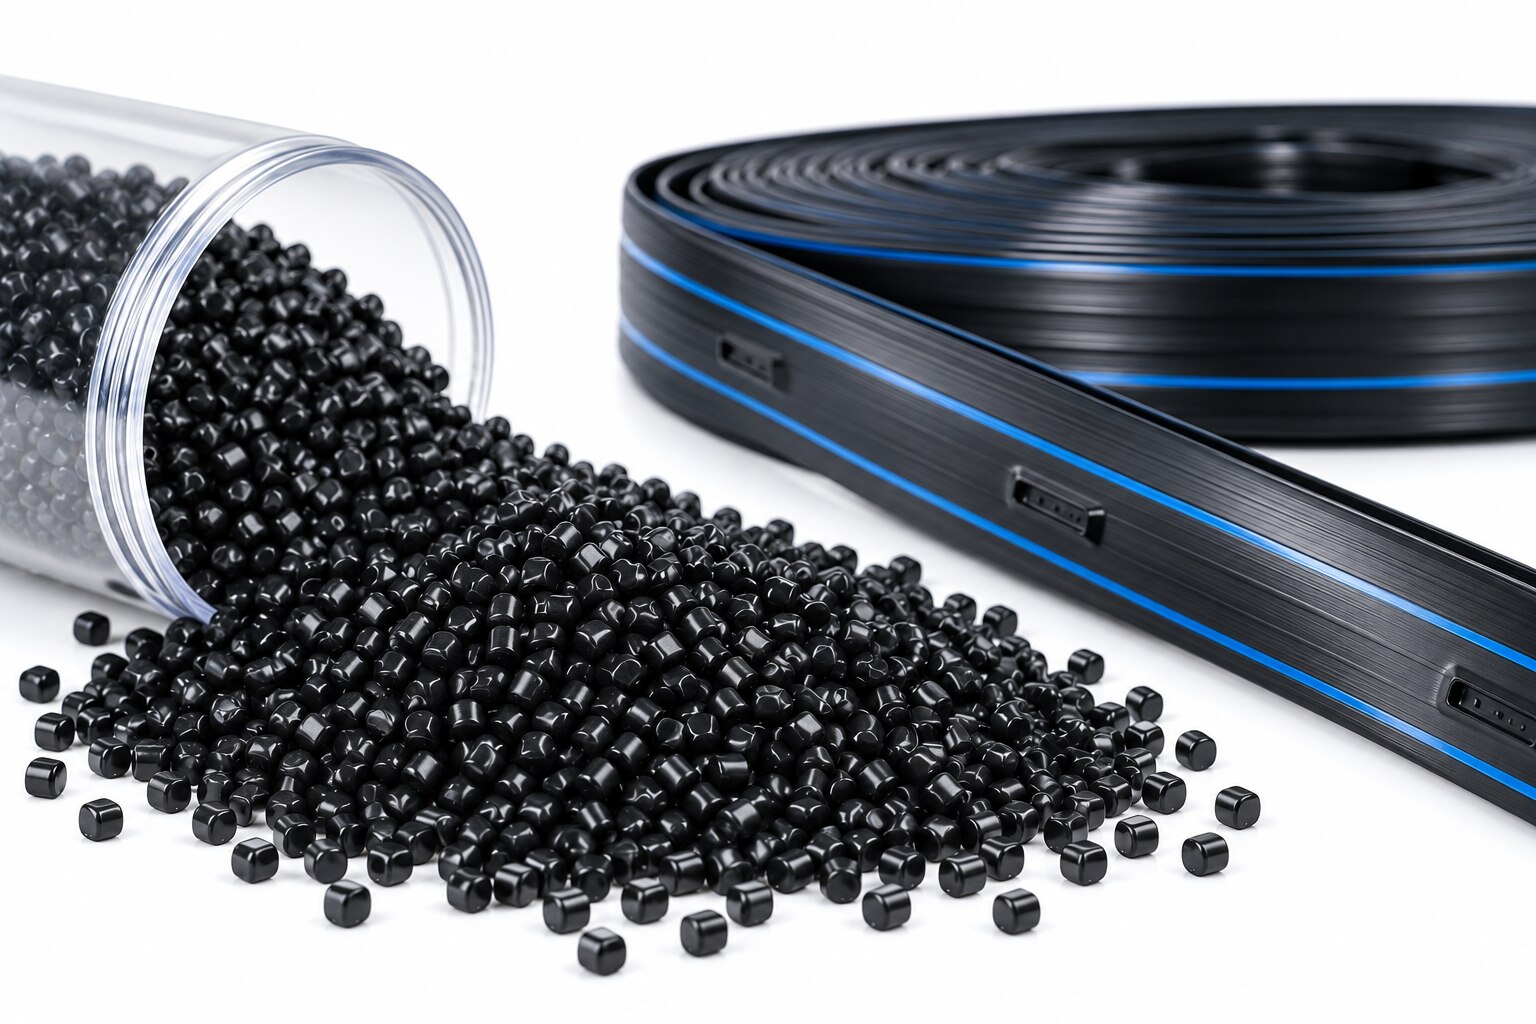
A flat drip pipe can show an acceptable black shade and still contain pigment agglomerates that become streaks, pinholes, weak zones or unstable extrusion. By the end, you will be able to connect dispersion with pipe performance, identify the production causes of defects, set a defensible let-down ratio and request evidence that a masterbatch works in your process.
Key takeaways
- Reject lots with visible agglomerates, streaks or uneven colour across the film.
- Check melt temperature, screw speed, back pressure and residence time during extrusion.
- Compare dosage against supplier data and request batch-specific dispersion evidence.
- Test finished pipe sections for colour consistency and agglomerate-related defects.
What good dispersion looks like inside a flat drip pipe
Good dispersion means carbon black, colour pigment or filler is distributed evenly through the thin PE film of a flat drip pipe, giving each section a comparable concentration. Colour alone is insufficient evidence: a drawdown can match the target shade while coarse agglomerates remain hidden or fall below visual detection.
Inspect the full tape width and length for these signs:
- Streaks and colour bands create uneven opacity and carbon-black distribution, leaving parts of the pipe less protected from sunlight.
- Specks and translucent zones reveal local concentration changes that become visible during folding, stress the seam and reduce sealing reliability.
- Coarse agglomerates act as thin-film defects, raising the risk of pinholes, tear initiation and brittle weak points in the finished pipe.
A visually acceptable drawdown can still contain defects large enough to form gels, die lines or weak points during extrusion. A drawdown also does not reproduce the thin wall, stretching, folding and seam-forming stresses of a flat drip pipe.
The correct question is whether the largest defect population remains harmless at the selected let-down ratio, not simply whether the sample looks black or evenly coloured. For filler concentrates, mineral particles can add roughness and brittle spots even when the overall shade appears consistent.
Good dispersion therefore supports opacity, sunlight protection, folding durability and seam integrity together.
Which extrusion conditions create poor dispersion?
Agglomeration begins when the melt cannot break down and distribute the concentrate. Inadequate melt mixing, an unsuitable screw speed, insufficient back pressure, excessive throughput or poor melt temperature leave pigment-rich pockets in the PE resin.
Excessive masterbatch addition increases viscosity and overloads the mixing section; moisture, contamination and a loaded or damaged screen pack add gels, pressure rises and unstable output.
| Condition | Production cause | Result |
|---|---|---|
| Incorrect screw or die conditions | Poor conveying, mixing or flow balance | Streaks, die lines and uneven distribution |
| Unsuitable screw speed | Too little shear or excessive residence time | Coarse agglomerates or thermal degradation |
| Low back pressure or excessive throughput | Insufficient dispersive mixing | Colour bands, specks and pressure fluctuation |
| Poor melt temperature control | Incomplete melting or overheated carrier | Unstable output and surface defects |
| Moisture, contamination or damaged screen pack | Gas, foreign particles or restricted flow | Gels, pinholes and screen-pressure rise |
Carrier-resin compatibility matters as much as pigment dispersion. Match the carrier to the PE pipe grade and its processing rheology; nominal melt-flow-rate matching is only a starting point. Molecular weight, polarity, pellet size and behaviour at the actual shear rate can still differ, causing phase separation, die build-up and surface defects.
The result can include pressure fluctuations, unstable output and lower weld or seam strength.
A supplier’s similar MFR does not prove compatibility. Confirm stable pressure, clean die surfaces and consistent output at the production let-down ratio before approving the concentrate.
How can you measure dispersion before approving a lot?
Approve a lot only after three checks, because good colour can hide coarse agglomerates that later produce gels, die lines or weak points.
1. Extrude tape at production settings and inspect its full width and length under consistent lighting. Look for streaks, specks, colour bands, translucent zones, gels and local opacity changes. Record each defect’s position instead of judging one short strip.
2. Cut and retain labelled samples from start-up, transition and steady-state output. Keep the lot number, sampling time, line speed and actual let-down ratio with each piece so a dispute can be tied to production conditions, not only to a supplier’s reference sample.
3. For a disputed lot, use microscopy or an agreed dispersion rating. ISO 18553 assesses pigment or carbon-black dispersion in polyolefin pipes, fittings and compounds. Put the required acceptance grade in the purchase specification; “uniform dispersion” alone is not a measurable pass criterion.
A controlled screen-pressure or filter-pressure trial adds process evidence. A rapid pressure rise can indicate contamination, agglomerates or poor melt filtration. Compare lots only when screen area, mesh sequence, melt temperature, throughput, residence time and actual let-down ratio remain constant; otherwise the screen-pack pressure result describes the test setup as much as the masterbatch.
What should you confirm about dosage and the supplier’s evidence?
A 40% carbon-black figure does not set the correct masterbatch dosage or let-down ratio. Dosage depends on the target opacity, flat-pipe wall thickness, base-resin colour and carbon-black efficiency. A thin black wall may need less concentrate than a pale, thicker wall, but only a controlled trial establishes the result.
At very low addition rates, feeder resolution becomes critical. An over-concentrated product can force the feeder below its stable operating range, causing short-term variation and local overdosing. The average formulation may be correct while streaks, viscosity changes or additive-rich regions appear in the tape.
Ask the supplier for:
- The technical data sheet, recommended let-down range and carrier-resin type.
- Carbon-black or filler content, expressed as a defined percentage, plus the moisture limit.
- The batch number linked to the supplied bags and certificate or test record.
- The colour or opacity target, test method and specimen thickness used to set that target.
- The processing window: melt-temperature range, feeder conditions and extrusion guidance.
- A retained production sample from the quoted batch, sealed and identified for later comparison.
Use these records to compare material from suppliers such as Khetan Polytex Private Limited at the same let-down ratio and feeder setting. Reject “very good dispersion” as a qualification result unless the supplier provides batch-linked evidence and the concentrate passes your microscopy, pressure-screen and finished-tape checks.
Related products
 | Black masterbatches black masterbatch(Diamond Black)(BU15050) ₹150 Specially designed for Drip Irrigation pipes like flat drip, round drip, in line and online. It contains P Type Black, Carbon loading 40%. View product → |
 | Black masterbatches BLACK MASTERBATCH Diamond black ₹150 Black masterbatch containing 40% carbon Black Content for Lateral pipes and Drip Irrigation Pipes View product → |
How do you prove dispersion in the finished flat drip pipe?
Approve a lot only after evidence survives three scales: microscopic inspection, a controlled process trial and testing on the finished flat drip pipe.
1. Examine cross-sections and film samples for carbon-black, pigment or mineral agglomerates. Record the microscope result against an agreed acceptance grade, using ISO 18553 where applicable. Retain samples from start-up, transition and steady-state production; a colour match alone cannot reveal brittle filler clusters or poorly dispersed additive-rich streaks.
2. Run the masterbatch at the agreed let-down ratio through the actual pipe formulation, keeping melt temperature, throughput, residence time, screen pack and pressure constant. A controlled extrusion or pressure-screen trial exposes contamination, pressure rise and incomplete breakup that a laboratory drawdown misses.
3. Test the finished pipe for tensile strength and elongation, leak or burst behaviour, seam integrity, folding performance, and flow or emitter performance where applicable. For emitting pipes, use the relevant requirements of ISO 9261; confirm seam strength and sealing after conditioning, because slip, antiblock and processing-aid migration can narrow the sealing window.
4. Treat black masterbatch as one part of protection, not a UV stabilisation package. Check the formulation, thermal history and base resin separately, then use an agreed accelerated-weathering or field-exposure protocol; ISO 4892 provides exposure methods, not a service-life guarantee.
Run separate checks for slip, antiblock, processing-aid and filler concentrates. Moisture, mineral agglomerates, migration and brittle spots can defeat a pipe that passes a colour check.
Frequently asked questions
What does good dispersion look like inside a flat drip pipe?
Carbon black, colour pigment or filler is distributed evenly through the thin PE film, giving each section a comparable concentration without coarse agglomerates.
Which extrusion conditions create poor dispersion?
Incorrect melt temperature, screw speed, back pressure, residence time or mixing conditions can leave pigment and filler agglomerates in the pipe film.
How can you measure dispersion before approving a lot?
Inspect drawdowns and extruded film for streaks, specks and agglomerates, then use a defined microscopy or dispersion-rating method rather than relying on colour alone.
What should you confirm about dosage and the supplier’s evidence?
Confirm the recommended dosage, carrier compatibility, batch identification and test evidence that supports the stated dispersion performance.
How do you prove dispersion in the finished flat drip pipe?
Sample sections from across the pipe and production run, then check colour consistency, film defects and agglomerates using the same acceptance method used for approval.